Machine longer.
Less carbide.
Cutting edges that last 60 % longer — reproducible on every cutting edge, in your grinding machine or in the K2E.
What the edge is worth Send a sampleThe difference at the edge
Every workpiece is raw material
Tungsten and cobalt are not getting cheaper. Anyone who manufactures or regrinds drills and milling cutters now buys tungsten carbide at a multiple of the price of early 2026.
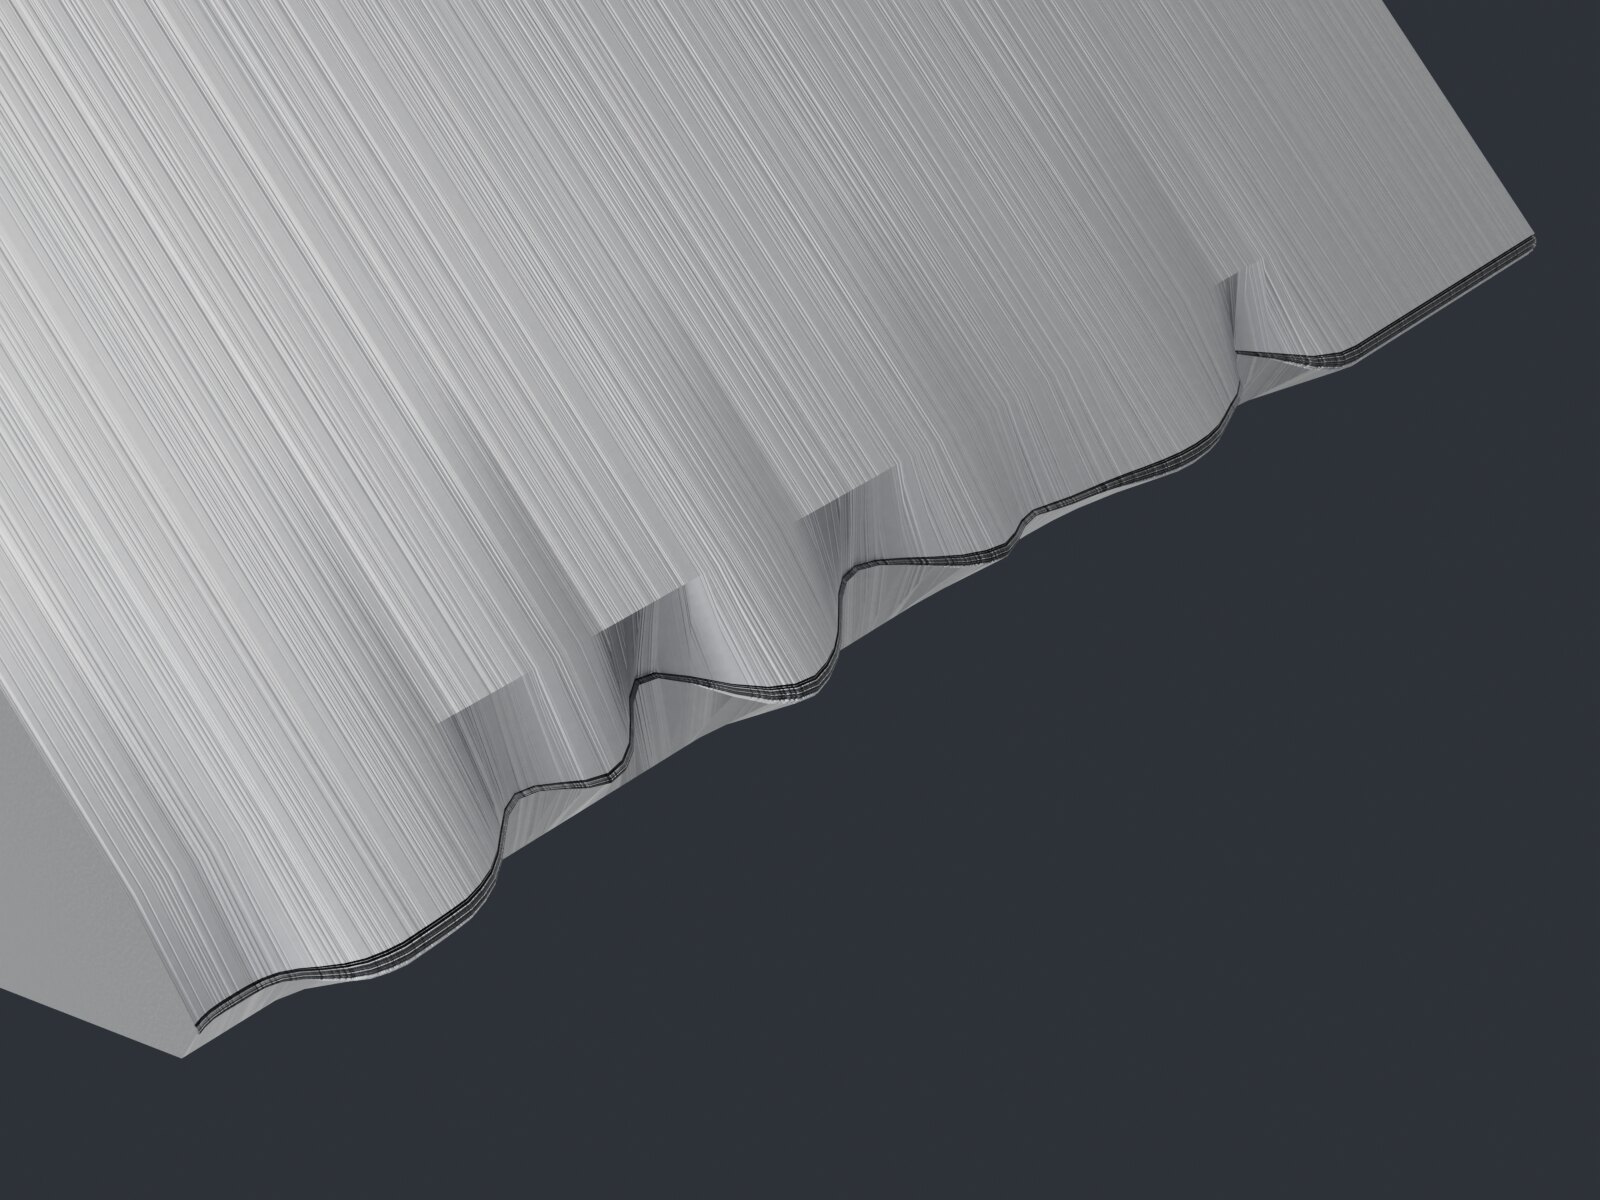
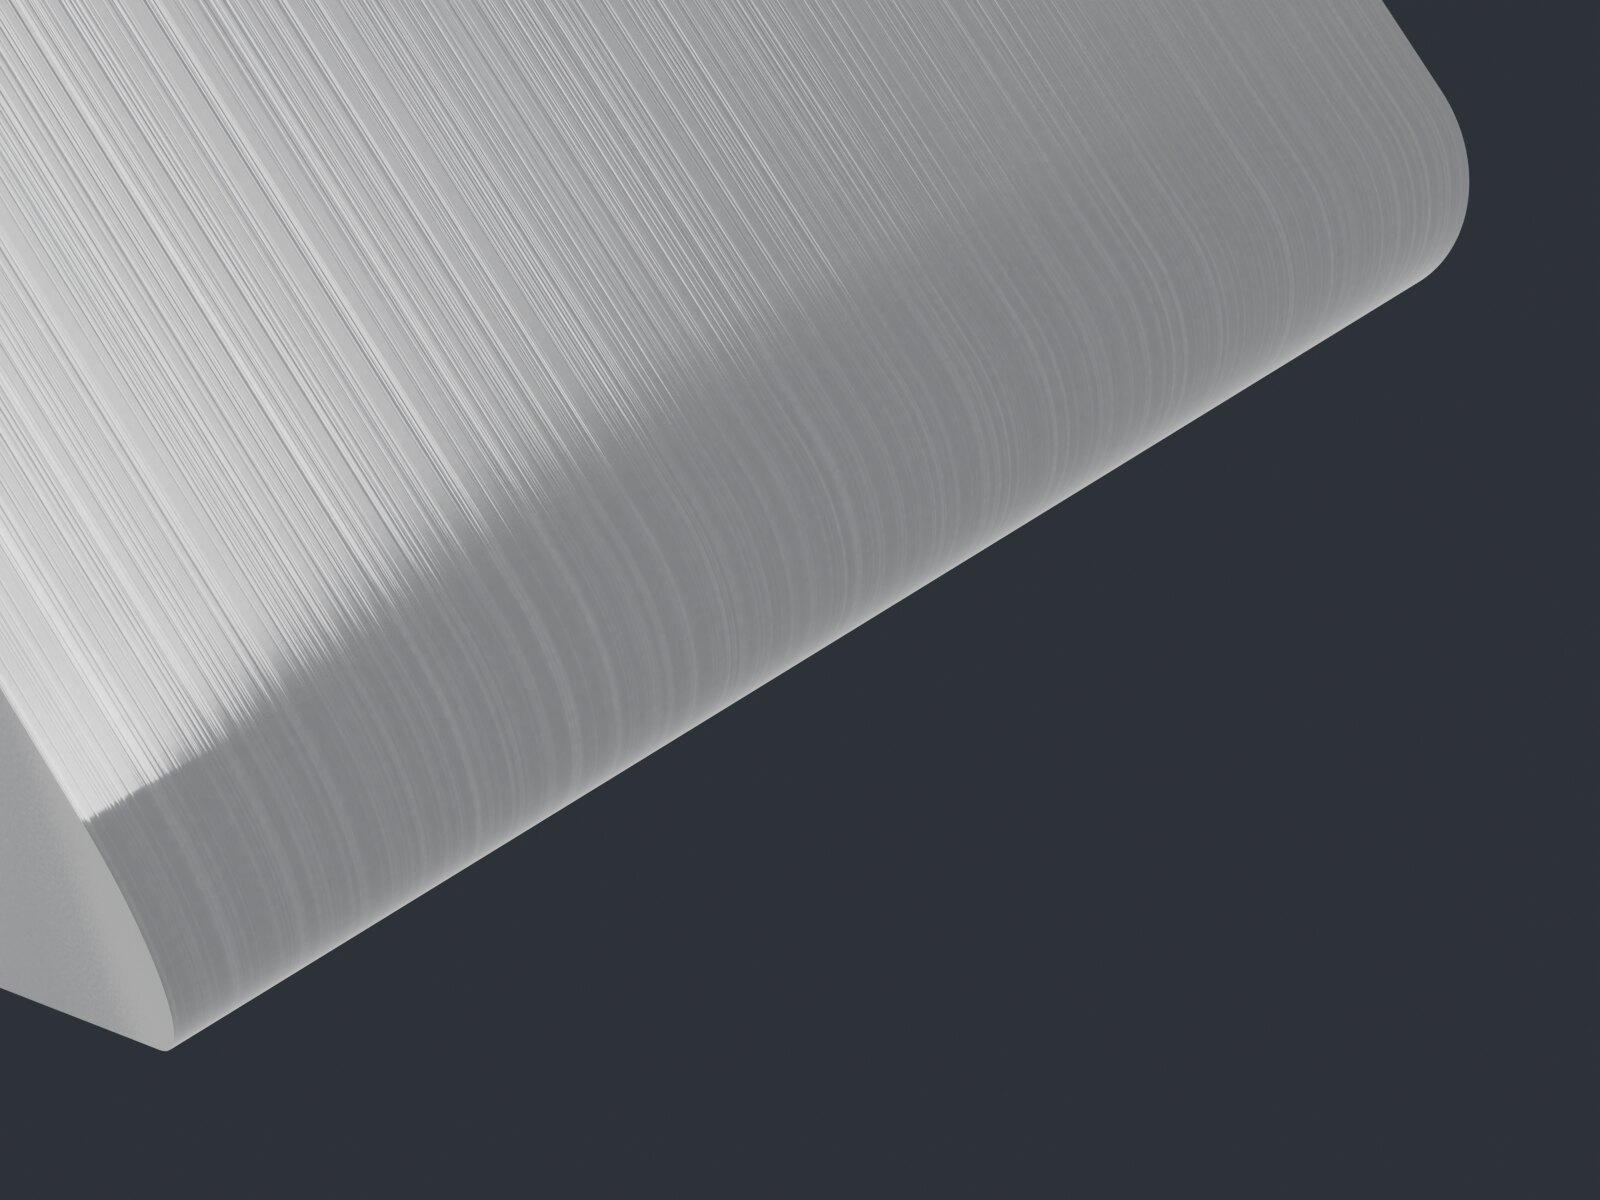
The biggest lever is not in purchasing but at the cutting edge: a sharply ground carbide edge chips microscopically at the first engagement. An edge rounded to a defined radius does not — it cuts evenly, wears later and lasts longer.
Fewer cutting tools – fewer regrinding cycles – less scrap. That is sustainability that pays off.
Sustainable machining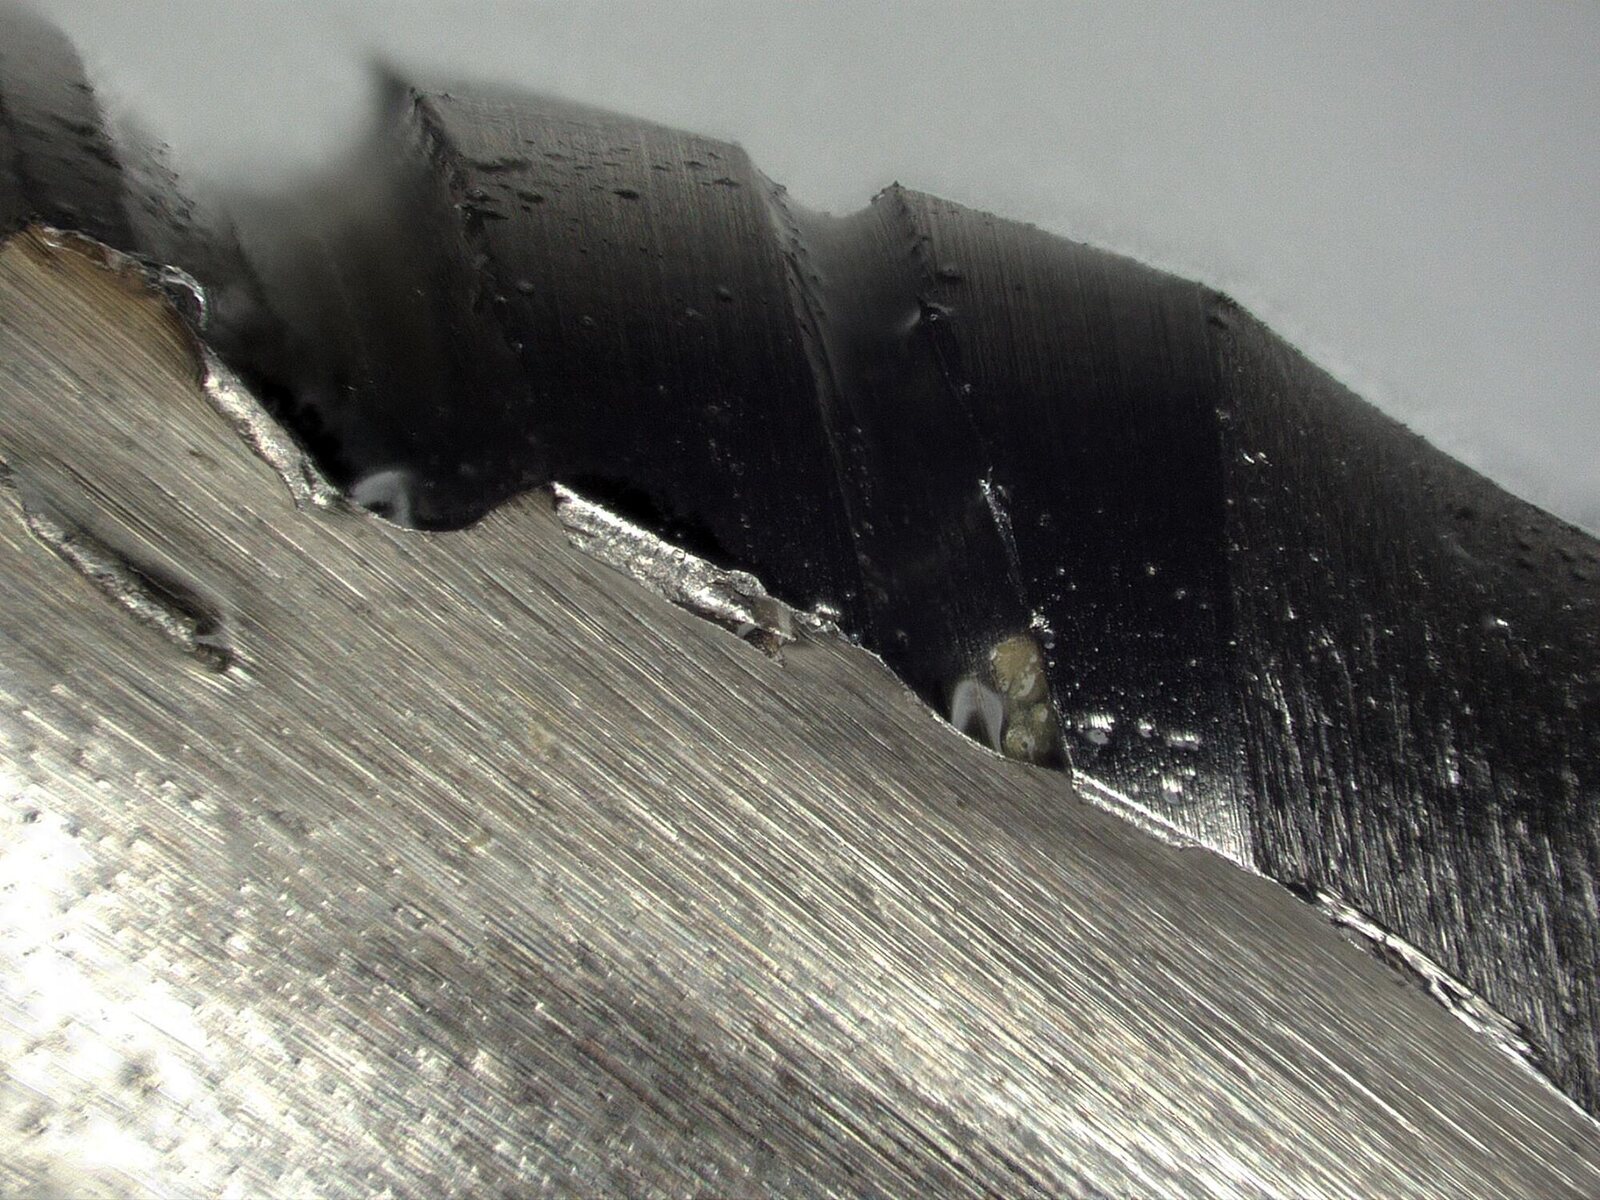
The same work. One third fewer cutting tools.
60 % longer tool life means: the same machining volume takes only 62.5 cutting tools instead of 100. Every cutting tool saved is not bought, not reground, not transported and causes no production stoppages.
Machine better, last longer, save raw material
One edge, two winners
The benefit is shared. Whoever manufactures or regrinds cutting tools sells a documented edge. Whoever machines with FLAKKOTING-treated cutting tools changes tools less often, has less downtime and produces less scrap.
- One third less carbide for the same machining work at the customer: 100 cutting tools become 62.5.
- Less scrap in your own production: a defined edge instead of a jagged one, every cutting edge the same — commercially available inserts vary by 20 to 50 µm along one cutting edge.
- A sales argument with a figure: radius, K-factor and tool life documented per workpiece. The data sheet replaces the promise.
- Regrinding at new-tool level: the reground drill gets the same edge as the new one.
- +60 % tool life in the customer test, up to +100 % in the technical literature: fewer tool changes, less downtime.
- Predictable wear instead of edge fracture: the change of cutting tools can be scheduled, less scrap and rework on the component.
- Process-reliable at high cutting values: uniform surfaces without chipping marks, Ra −30 % measured in drilling.
- Less raw material per component: 37 % fewer cutting tools bought, stored, transported, disposed of.
Three routes to a better edge
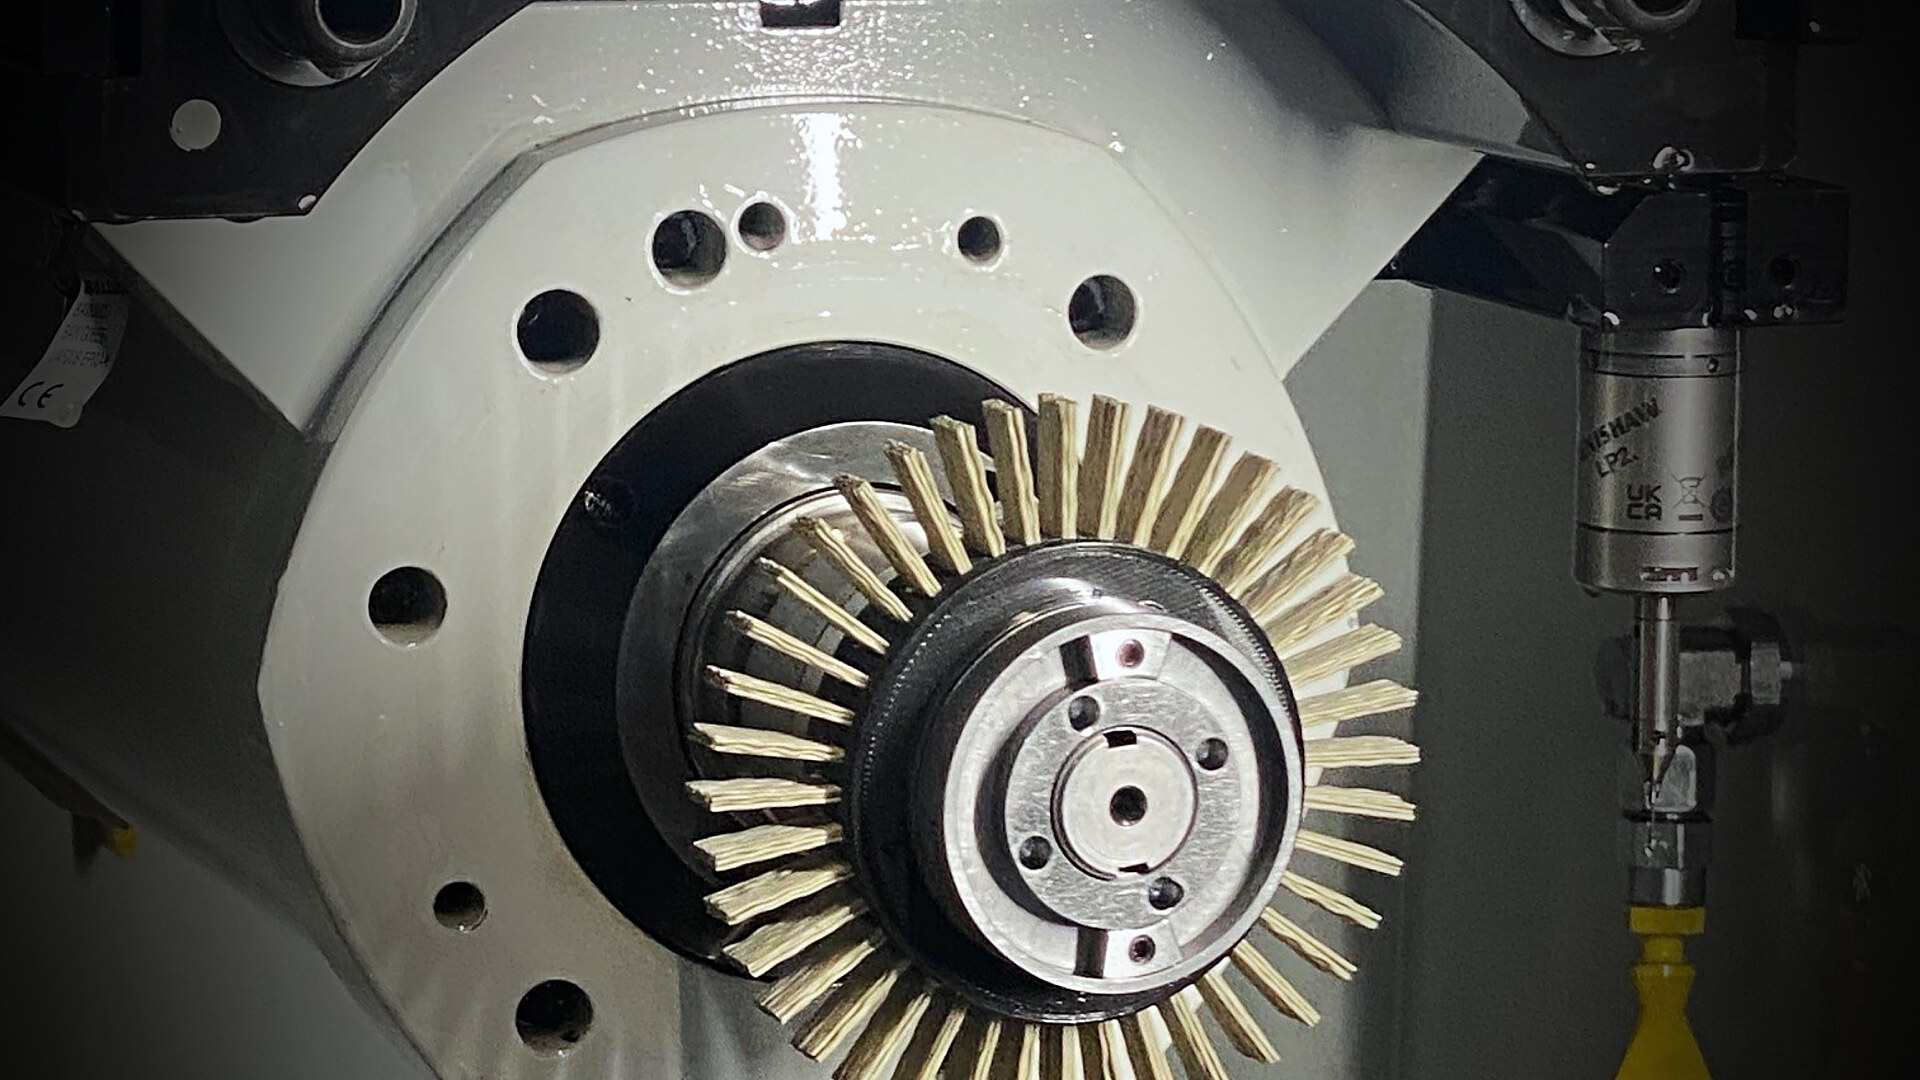
Cutting tool manufacturers
Edge preparation directly in the grinding machine, 10–40 seconds per workpiece, parameters from MIKRO-KI.
More →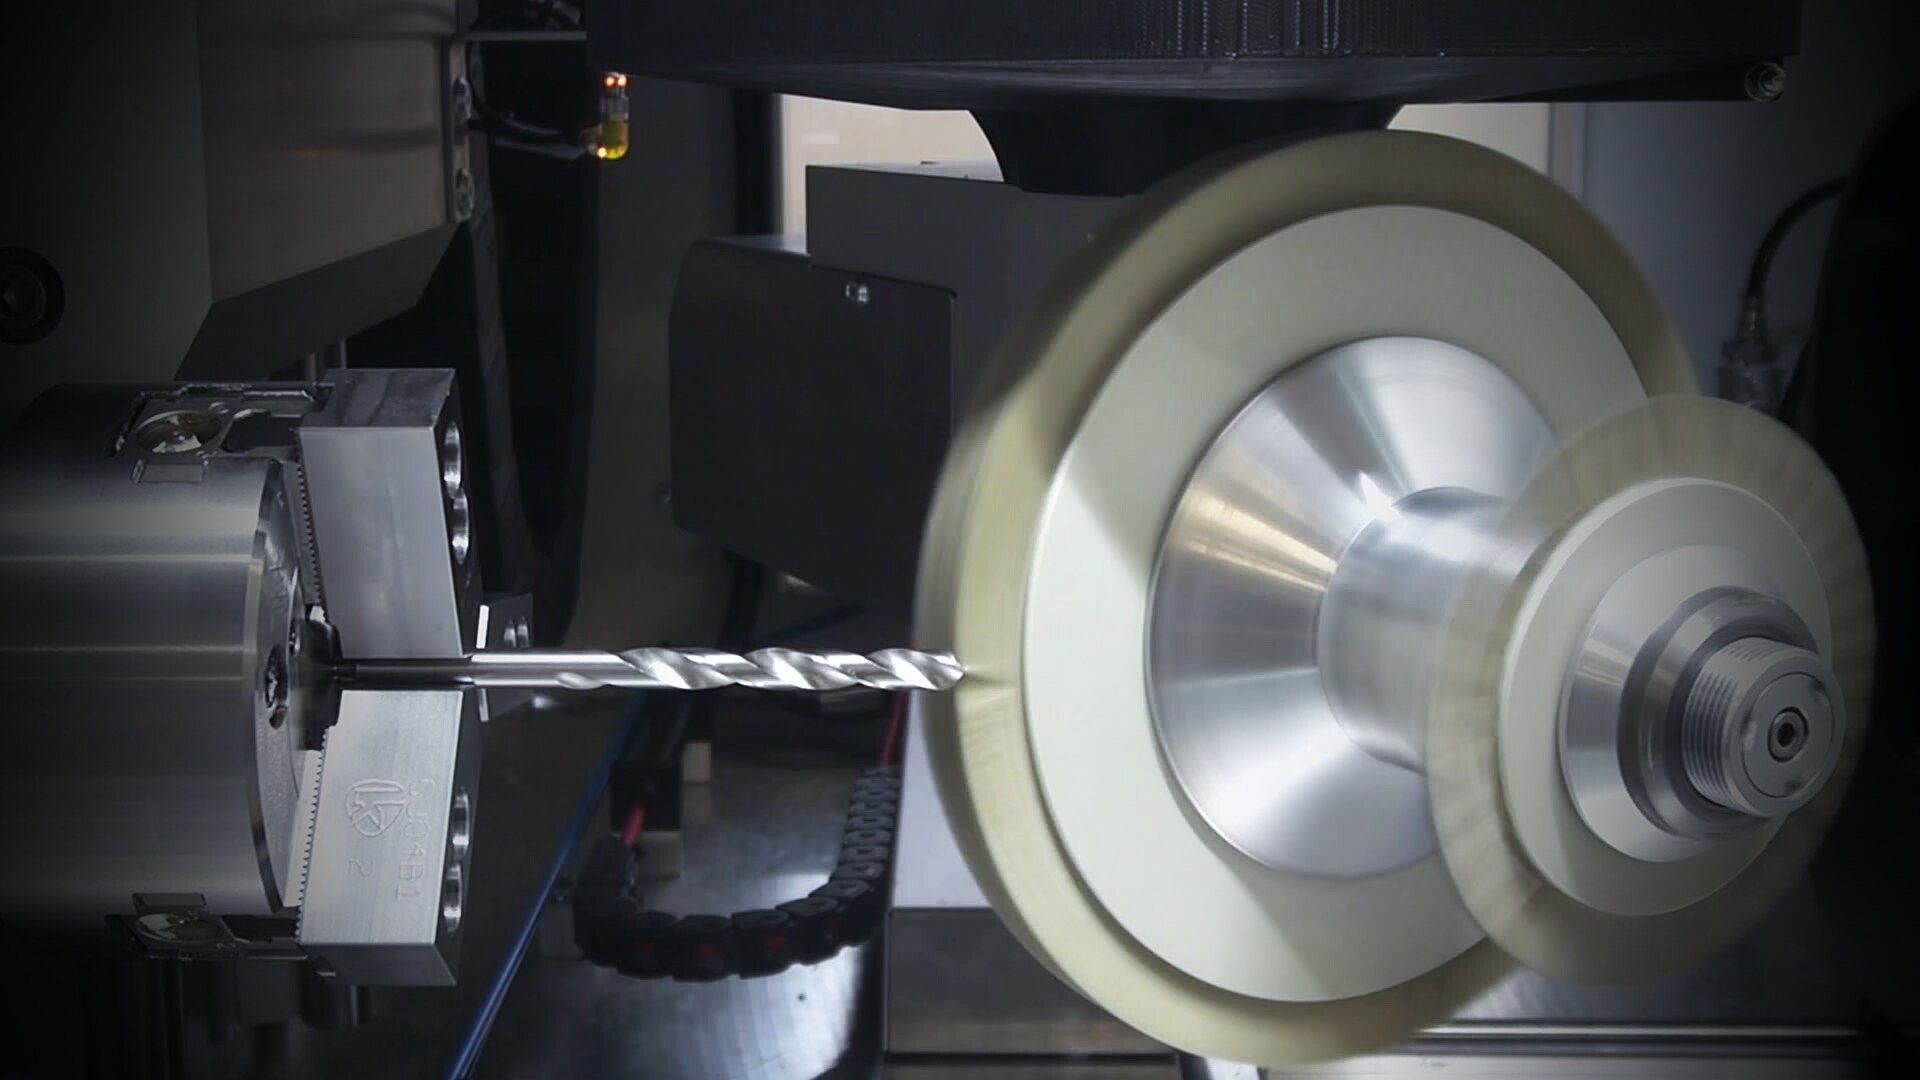
Regrinding shops & complex workpieces
Step drills, form milling cutters, taps: many cutting edges, different radii. The K2E prepares every cutting edge in a single clamping — 2–3 minutes per workpiece, reground as good as new.
More →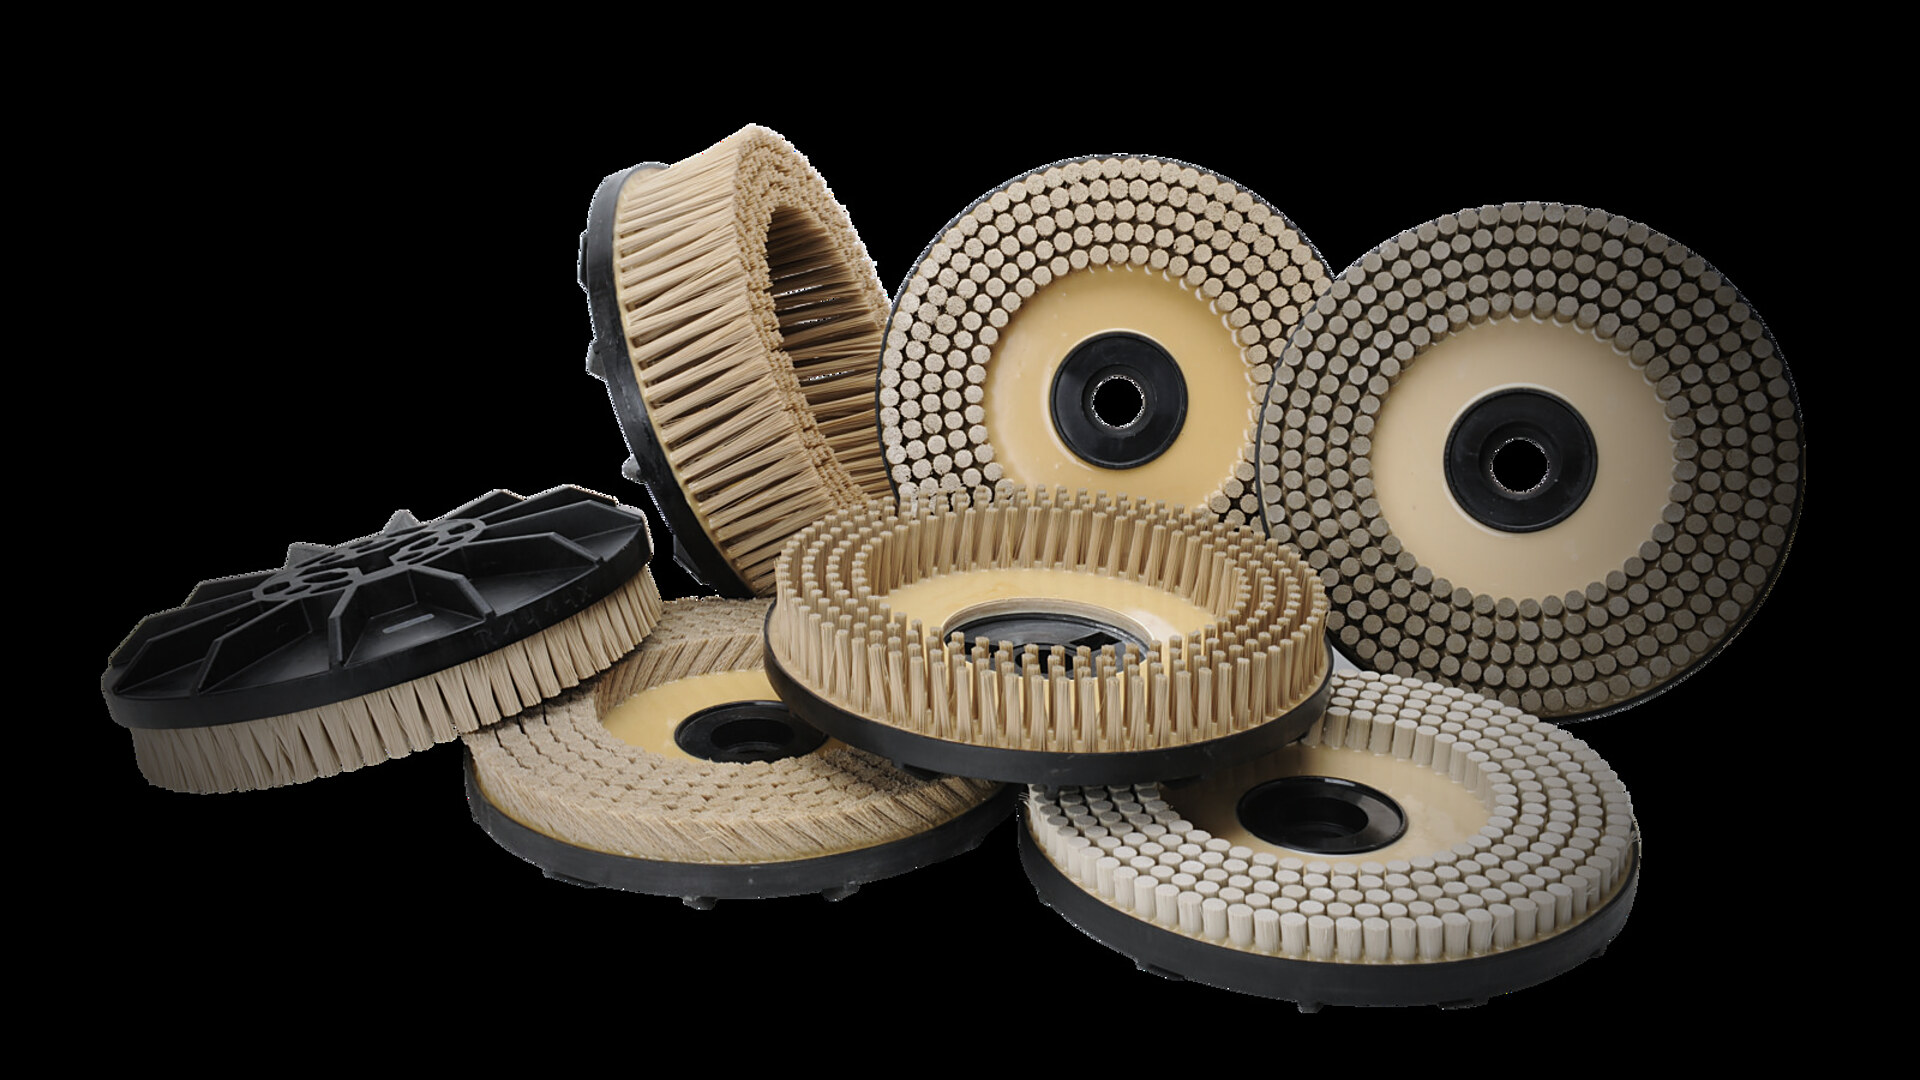
Machine builders & OEMs
You integrate FLAKKOTING into your grinding or handling machine. PROFIN supplies the FLAKKOTING tools, the process parameters and the MIKRO-KI model.
More →Process, model, machine
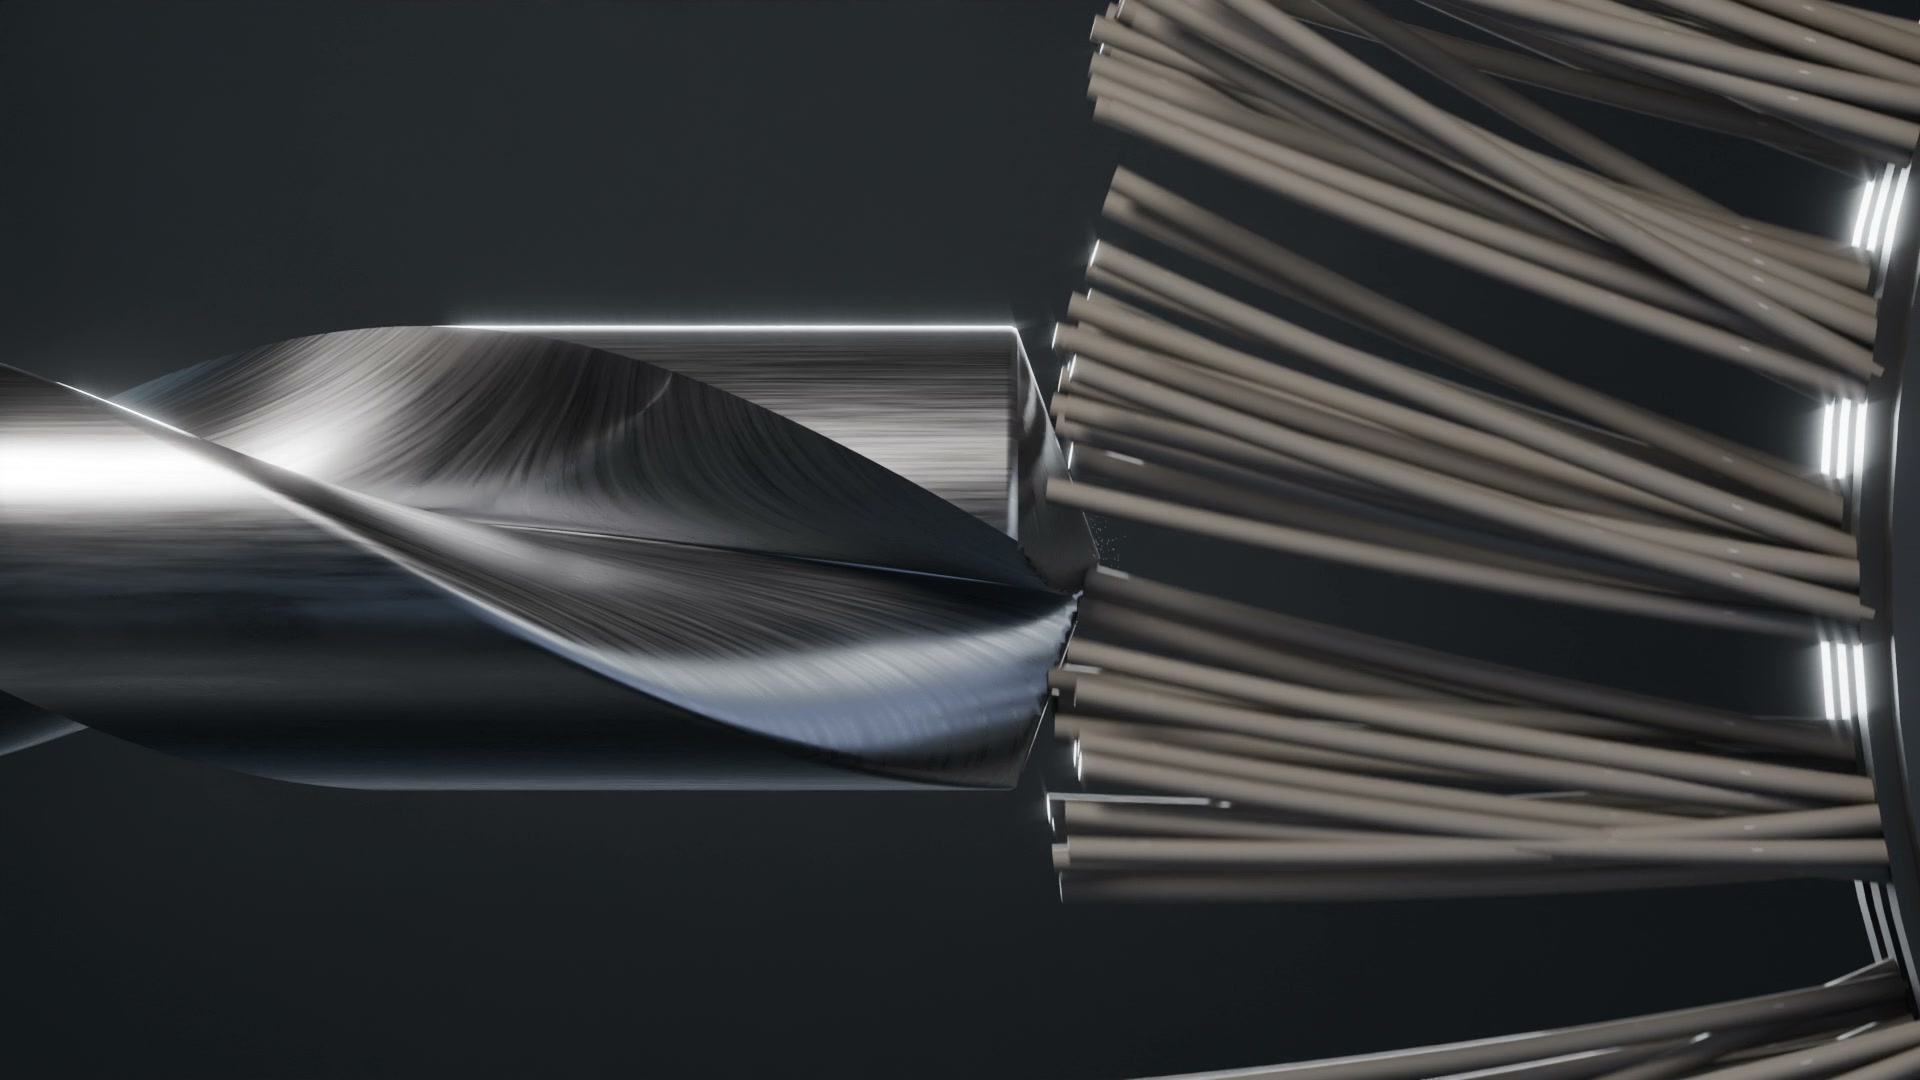
FLAKKOTING
The cold ultra-fine grinding process with diamond filaments: radii from 5 to 50 µm, edge shape according to K-factor.
The process →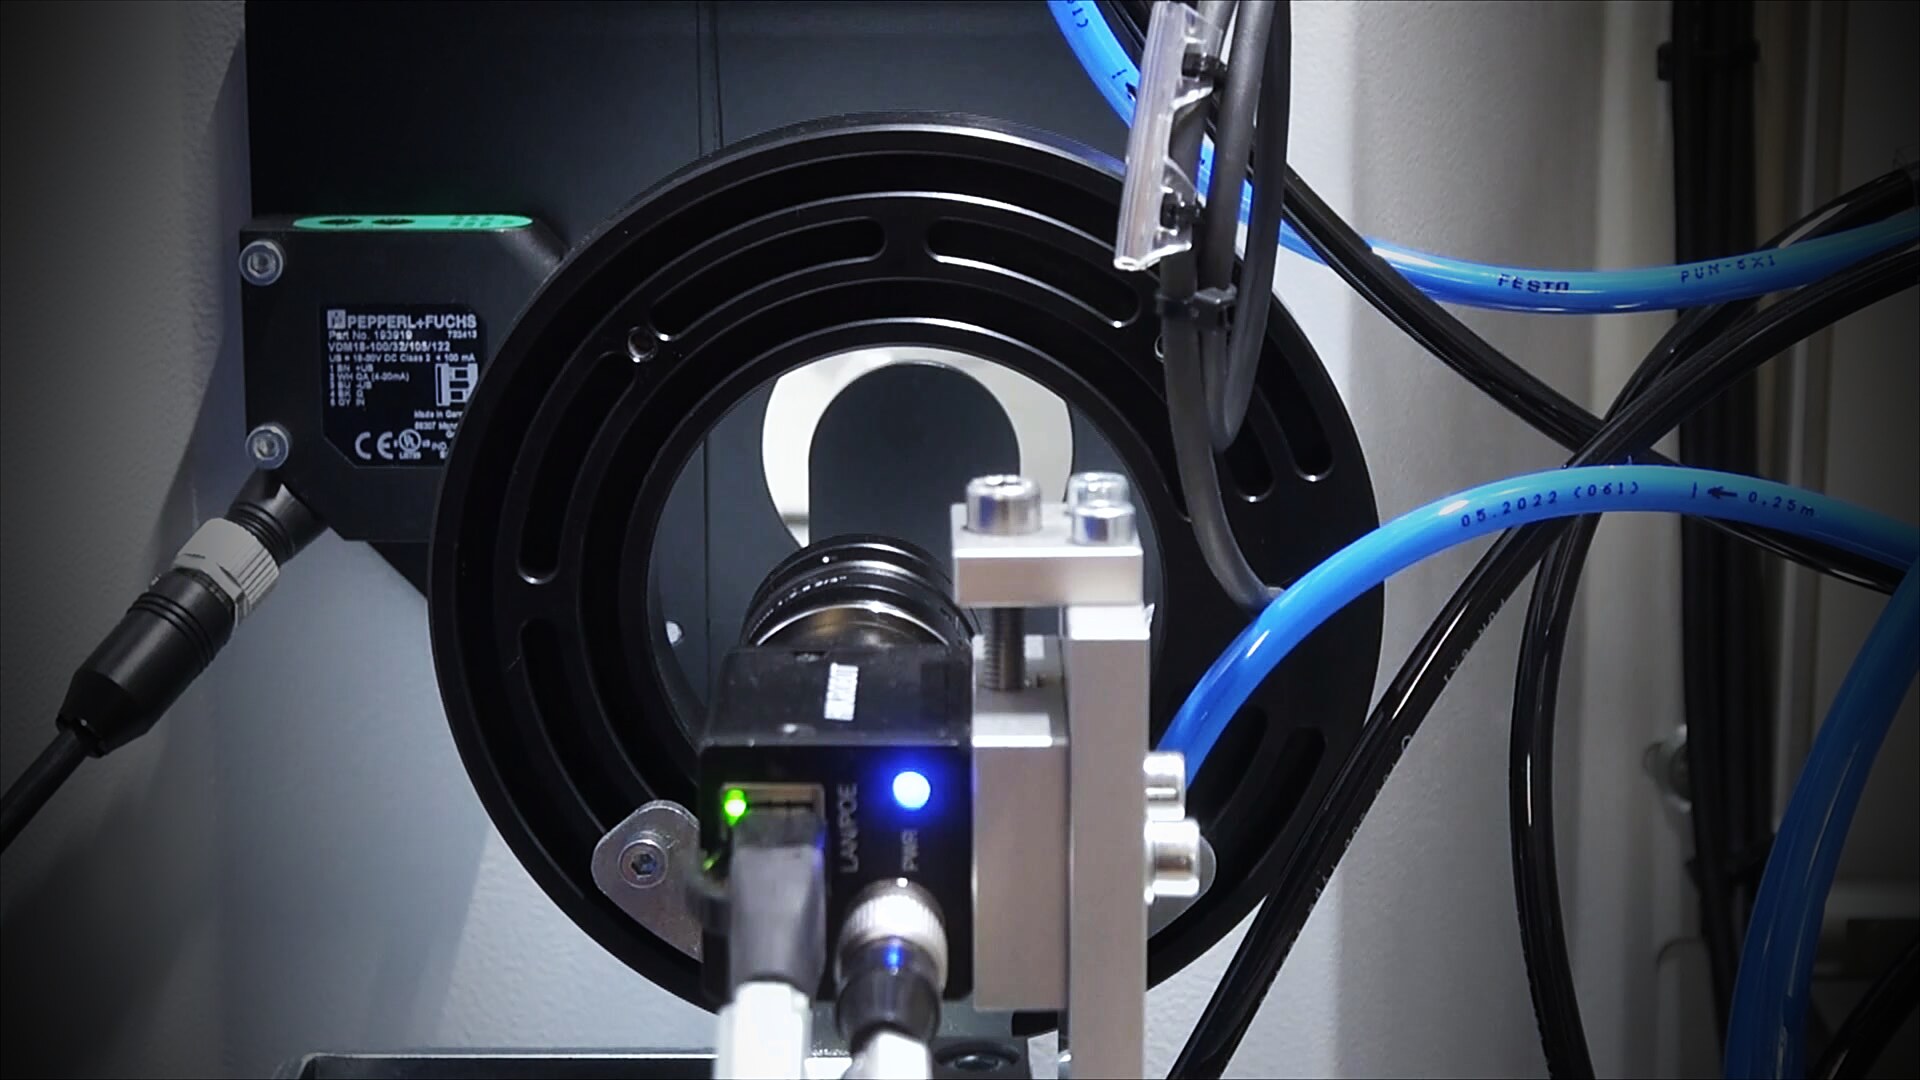
INNOFLAKK with MIKRO-KI
Enter the target radius and the workpiece — the model built from several thousand measured edges supplies the process parameters.
The model →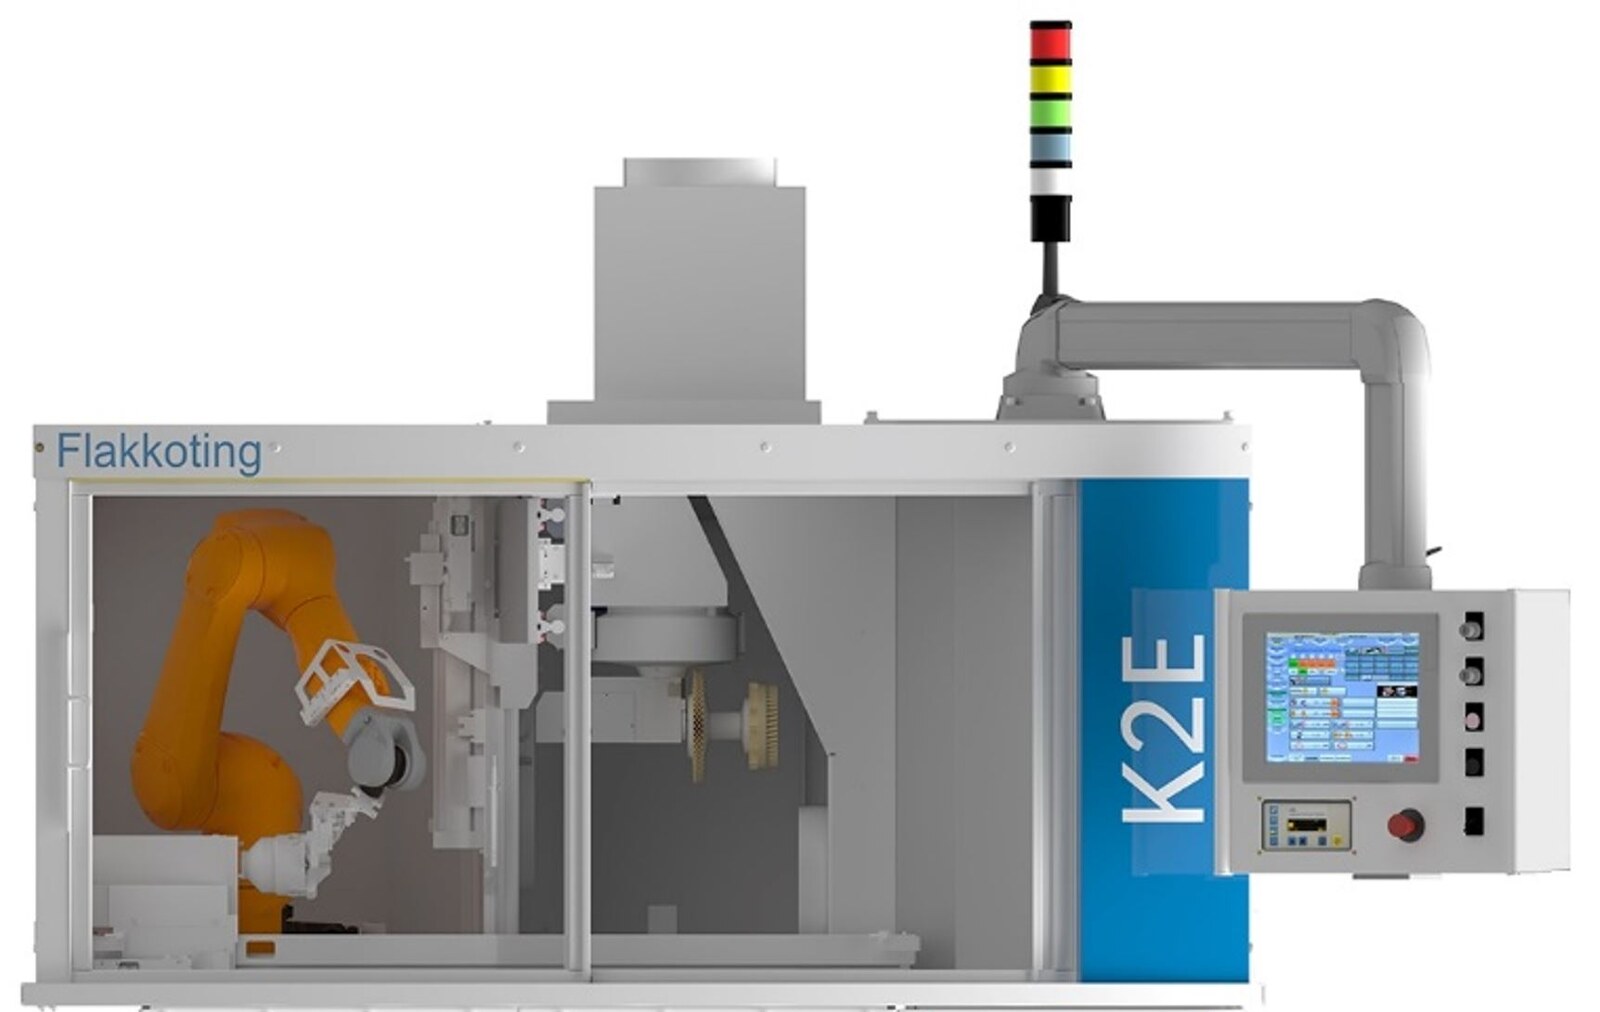
K2E family
The 6-axis centre for micro cutting edges on cutting tools — from manual operation to series production with a robot.
The machine →
 Research partner affiliated with ETH Zurich
Talks: Arbeitskreis Hartmetall 2026 · Schleifsymposium 2026
Send us a workpiece.
We prepare it, measure the edge and show you what the edge is worth in your process.
Tool sample processing
You send us your workpiece, we treat it by FLAKKOTING in the process laboratory in Littau and you receive the measured results: radius, K-factor and images of the edge. First results from approx. CHF 800, FLAKKOTING day with documentation on request.